1. Introduction: Pulse Architecture & Laser Physics
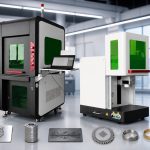
When investing in industrial fiber laser marking equipment, the choice between MOPA (Master Oscillator Power Amplifier) and traditional Q-Switched lasers represents the most critical architectural decision. While both operate at a standard wavelength of 1064 nm and are designed for high-speed precision processing on metals and engineered polymers, their internal beam pulse control mechanisms differ fundamentally.
Traditional Q-switched lasers (such as standard Raycus, MAX, or IPG YLP sources) utilize an acoustic-optic or electro-optic Q-switch to generate high-energy laser pulses. However, their pulse duration (pulse width) is inherently fixed—typically between 80 ns and 140 ns—and cannot be modulated independently of pulse repetition frequency (PRF).
In contrast, MOPA fiber lasers (led by JPT M7/M8 and IPG-M series) separate the seed laser (Master Oscillator) from the optical amplifier stage (Power Amplifier). This decoupled architecture empowers engineers and operators to independently adjust:
- Pulse Duration / Pulse Width: Ranging dynamically from 2 ns to 500 ns.
- Pulse Frequency (PRF): Ranging from 1 kHz to 4000 kHz (4 MHz).
- Peak Pulse Power & Single Pulse Energy: Maintained consistently even at extreme high-frequency cycles.
2. Key Technical Differences: MOPA vs. Q-Switched
| Engineering Parameter | Standard Q-Switched Laser (Raycus/MAX) | Advanced MOPA Laser (JPT M7/M8) | Practical Application Impact |
|---|---|---|---|
| Pulse Duration (Width) | Fixed (~80 ns – 120 ns) | Adjustable (2 ns – 500 ns) | Short pulses (2–10 ns) eliminate thermal burning on delicate substrates; long pulses maximize deep engraving. |
| Pulse Frequency Range | 20 kHz – 80 kHz | 1 kHz – 4000 kHz (4 MHz) | High PRF allows ultra-smooth continuous shading, color generation, and micro-machining. |
| Heat-Affected Zone (HAZ) | Moderate to High | Ultra-Low / Cold Processing | Prevents substrate deformation, warping, or yellowing on thin foils and plastics. |
| Stainless Steel Color Marking | Limited / Inconsistent | Full Spectrum (30+ Vibrant Colors) | Precise control of thermal oxide layer thickness creates reproducible interference colors. |
| Anodized Aluminum Marking | White / Grey frosted finish only | True Deep Black & Pure White | Sub-micron pulse spacing alters surface oxide micro-texture without breaching the conductive barrier layer. |
| Plastic & Polymer Processing | Frequent foaming or burning | Clean, High-Contrast Marking | Non-damaging photochemical reaction on ABS, PVC, PBT, and Silicon. |
| Equipment Capital Cost | Cost-effective baseline | Premium Tier (High ROI) | Higher upfront investment offset by 3x broader application capability and higher job margins. |
3. High-Value Industrial Application Capabilities
A. Color Laser Marking on Stainless Steel & Titanium
Color marking on stainless steel (AISI 304/316) is achieved through controlled thermal oxidation that forms a transparent dielectric oxide film. When light reflects off both the top surface of the oxide and the metal substrate below, constructive and destructive optical interference produces vivid colors across the spectrum.
Why MOPA is mandatory: Generating repeatable colors requires precise nanoscale control over the oxide layer thickness (between 50 nm and 350 nm). MOPA lasers achieve this by setting ultra-narrow pulse durations (4–20 ns) at high frequencies (150–500 kHz), fine-tuning energy density without scorching the metal.
B. True Black Marking on Anodized Aluminum
In consumer electronics, aerospace, and medical device manufacturing, laser marking on anodized aluminum must produce a high-contrast matte black mark without damaging the anodized protective layer.
The MOPA Advantage: Using narrow pulse widths (2–15 ns) with tight line spacing (0.001 mm), MOPA creates light-trapping micro-craters in the oxide layer. Q-switched lasers, due to their wide 100 ns pulses, vaporize the anodized layer and expose the raw aluminum, leaving only a pale grey or white mark.
C. Thermal-Sensitive Plastics & Electronics
For IC chips, electronics packaging, medical syringes, and flame-retardant plastics, conventional lasers induce excessive thermal melting that destroys legibility. MOPA’s ultra-short 2 ns pulses operate below the thermal diffusion threshold, inducing photochemical color change without melting or burring.
4. Frequently Asked Questions (FAQ)
Q1: Can a Q-switched fiber laser produce colors on stainless steel?
Answer: While a Q-switched laser can occasionally produce faint brownish hues under very narrow laboratory parameters, it cannot reliably or consistently reproduce vibrant color spectrums due to pulse width instability. For commercial color marking, a MOPA laser is strictly required.
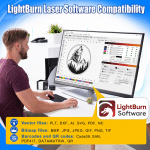
Q2: Is LightBurn compatible with MOPA fiber laser marking machines?
Answer: Yes! Modern MOPA fiber lasers equipped with standard JCZ (EzCad2) or compatible controllers can be operated seamlessly with LightBurn Laser Software, allowing full vector design, layer speed/power/frequency management, and direct Galvo control.
Q3: What is the ROI payback period for upgrading from Q-switched to MOPA?
Answer: For commercial job shops and contract manufacturers, MOPA machines command a 35% to 60% premium per engraving service because they can process anodized aluminum black marking, color jewelry personalization, and medical-grade UDI barcodes. Typical capital cost payback is achieved within 4 to 6 months.
5. Related Technical Documentation & Resource Downloads
- ActionLasers™ 2026 Complete Product Catalog (PDF Download) – Explore our full series of Fiber, CO2, and UV laser machinery.
- LightBurn Laser Software Full Setup & Download Guide – Complete tutorial for DSP & Galvo laser control.
- Ruida RDWorks V8 & CorelLaser Software Installation Guide – Troubleshooting & parameter backup manual.
- CO2 Laser Optical Path Alignment Guide – 3-Mirror alignment SOP and focal height calibration.